Nullam dignissim, ante scelerisque the is euismod fermentum odio sem semper the is erat, a feugiat leo urna eget eros. Duis Aenean a imperdiet risus.
Nullam dignissim, ante scelerisque the is euismod fermentum odio sem semper the is erat, a feugiat leo urna eget eros. Duis Aenean a imperdiet risus.
 Violet Feng
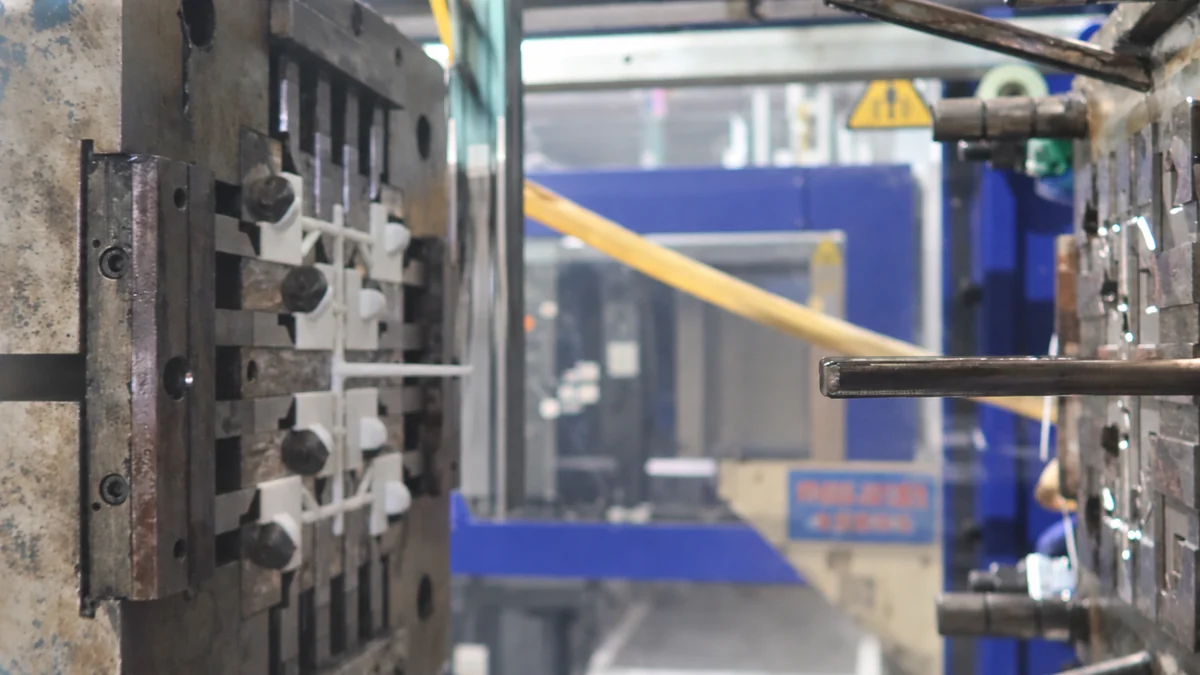
Injection molding cost has two layers: the one-time mold investment and the recurring cost of each part. A low tooling quote may not create the lowest total cost if it requires manual work, produces a long cycle, or cannot support the expected production life. A higher initial investment may be economical when multiple cavities or better cooling reduces the cost per unit.
A supplier cannot price a custom project accurately from quantity alone. The estimate must reflect CAD geometry, resin, tolerances, appearance, forecast volume, inspection, and work after molding. Shenyue’s plastic injection molding service connects these inputs from design review through repeat production. The ten factors below explain why quotes vary and what buyers should define before comparing them.
Total project cost combines tooling and validation with recurring production. Tooling covers design, mold material, machining, components, assembly, and trials. Production cost includes resin, machine time, labor, quality control, scrap, secondary work, and packaging. Buyers should also confirm whether freight, duties, and special documentation are included.
Buyers should ask how mold design affects cycle time, yield, maintenance, and unit price across the expected lifetime volume. This makes quotations easier to compare.
Several cost drivers affect both the mold and the molded part. The strongest quotation explains the assumptions behind them instead of presenting one unexplained total.

A larger part needs a larger cavity, mold base, and often a higher-tonnage machine. It also changes resin use, cooling demand, handling, and packaging. The mold must still provide space for runners, cooling, ejection, and moving mechanisms.
A straight-pull part can use a simpler mold than one with side holes, hooks, threads, or deep undercuts. Slides, lifters, collapsible cores, and hand-loaded inserts add components and maintenance. They may also extend the molding cycle.
Mold material depends on expected volume, resin behavior, surface requirements, and maintenance. Abrasive fillers or corrosive resins may require more resistant steel or treatment. Shenyue develops custom injection mold tooling around the part, resin, cavity strategy, and quality requirements. Selecting steel only by initial price can shift cost into wear or repair later.
A single-cavity mold usually costs less initially but produces one part per cycle. A multi-cavity mold costs more to build yet spreads machine time across several parts. The best cavity count depends on demand, machine capacity, runner balance, and quality risk.
Cold runners are simpler but create material that must be separated, recycled when allowed, or discarded. Hot runners can reduce waste and support more cavities, but add controls and maintenance. Gate type and location also affect appearance, filling, weld lines, and trimming.
Tight tolerances and demanding finishes require precise machining, stable processing, inspection, and sometimes mold adjustment. Texture, polishing, critical shutoffs, and gate restrictions also affect construction and scrap risk. Buyers should mark critical dimensions and cosmetic zones instead of applying the strictest requirement everywhere.
Material cost includes more than finished part weight. It may include runners, sprues, purging, startup scrap, color changes, moisture control, and unusable regrind. Commodity, reinforced, flame-retardant, and high-temperature resins also differ in price and processing behavior.
Machine cost is usually allocated by time. Thick sections, long flow paths, slow cooling, difficult ejection, and manual handling lengthen the cycle. Part size and projected pressure determine machine capacity. A short, stable cycle can matter more than a small resin price difference.
Inspection adds value when tied to function and risk. Dedicated gauges, dimensional checks, color standards, testing, traceability, and detailed reports require equipment and labor. Agree these requirements during quotation so suppliers do not price different quality scopes.
Printing, drilling, tapping, hardware insertion, assembly, and packaging change the delivered cost. Keeping secondary operations for molded parts within one project may reduce handoffs, but each operation still needs a method, acceptance standard, and volume assumption. Compare delivered-part cost rather than molding price alone.
Tooling is a fixed investment, while production costs repeat with each cycle. As lifetime volume increases, mold cost is spread across more parts. Higher volume may justify more cavities, automation, or a hot runner when production savings exceed the added tooling cost.
Use realistic order quantities, annual demand, and expected product life. An aggressive forecast can lead to an unnecessarily expensive mold, while an underestimated forecast can leave a slow tool unable to meet demand economically. Request several quantity breaks when demand is uncertain.
Two quotations may differ because they use different technical assumptions rather than different margins. Before choosing a supplier, confirm the following items in writing.
A quote that defines these items gives procurement and engineering teams a sound basis for evaluating total cost. A lower number with missing assumptions can become more expensive after tool changes, quality disputes, or unexpected downstream work.
Cost reduction is most effective before steel is cut. A practical mold design and engineering review can identify unnecessary undercuts, thick sections, difficult shutoffs, and requirements that lack a functional reason. The goal is to remove cost while keeping the part’s fit, function, appearance, and expected life.
An accurate injection molding quote depends on complete, controlled input. Buyers should prepare the following information before requesting a final price.
Open questions should be identified rather than hidden inside a generic specification. That allows the supplier to separate fixed requirements from preferences and present options with clear cost consequences.
Injection molding cost reflects part design, mold construction, material, cycle time, quality, and production volume. Define these inputs early and compare total delivered cost instead of one tooling number. Shenyue supports design review, tooling, sampling, production, and optional finishing.
Custom project cost depends on CAD geometry, part size, mold construction, resin, cavity count, tolerances, volume, quality scope, and secondary operations.
Quotes may assume different mold materials, cavity counts, runner systems, tool life, inspection, or included services. Compare the written technical assumptions.
Higher volume often spreads tooling and setup across more parts, but cycle time, cavity count, yield, material use, and maintenance still control the result.
Review the design before tooling, remove unnecessary undercuts, keep wall thickness consistent, define functional tolerances, and confirm material and appearance requirements early.
For a project-specific review, send the 3D model, drawing, material requirements, expected volume, and critical quality requirements to contact the Shenyue technical team. Shenyue can identify missing inputs and discuss a suitable tooling and production route.