Никакого достоинства, перед склериском - это euismod Fermentum ненависть. sem semper the is Erat, a feugiat leo urna eget eros. Дуис Энеан Стрижка для смеха.
Никакого достоинства, перед склериском - это euismod Fermentum ненависть. sem semper the is Erat, a feugiat leo urna eget eros. Дуис Энеан Стрижка для смеха.
 Вайолет Фэн
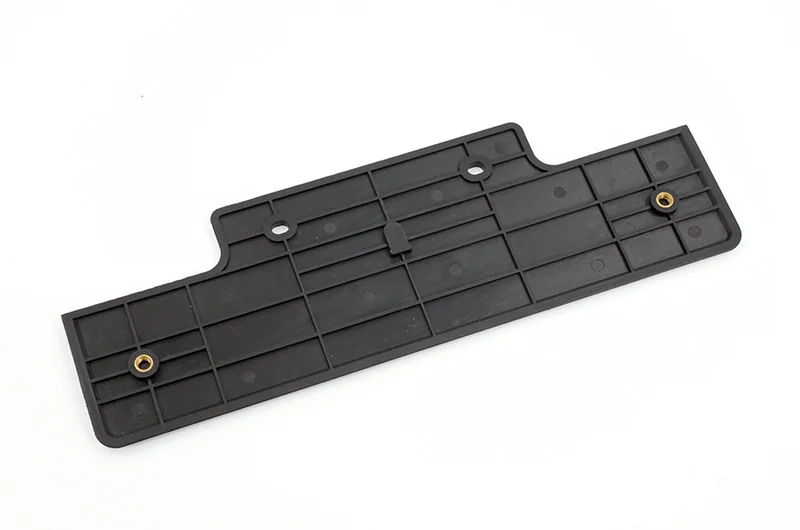
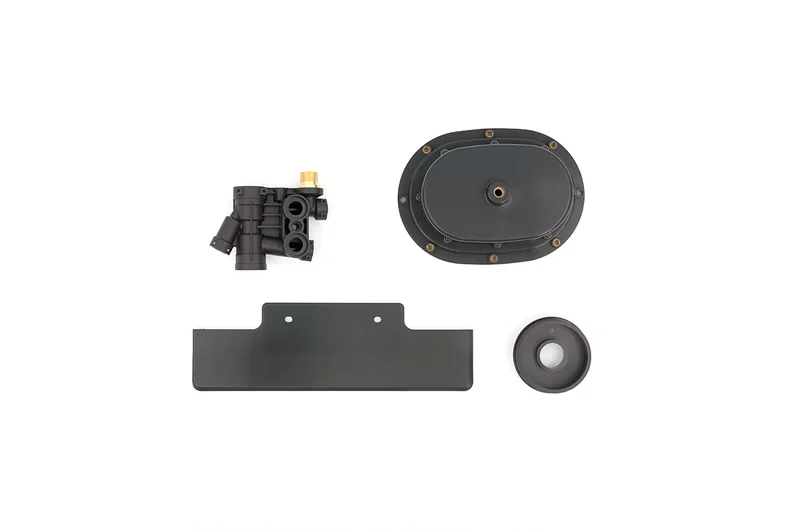
A molded housing can look complete and still fail a fit check. A mounting feature may sit too close to an edge, or a cover may pull inward after cooling. Before changing the mold, it is worth checking how the part was packed.
Holding pressure in injection molding helps compensate for material shrinkage while additional melt can still enter the cavity. Too little packing can leave sink marks and undersized features. Too much can create stress or make the part harder to eject. The useful question is not simply whether pressure should go up or down, but whether the right amount reaches the affected area for long enough.
During filling, the machine pushes molten plastic into the cavity. It then changes from filling control to the packing and holding stage. Pressure continues to act as the plastic cools, allowing more material to enter through the gate, the small opening that feeds the part.
Packing and holding are closely related. Packing adds material after the initial fill; holding maintains pressure as the gate seals. Machine programs may separate these stages or use a pressure profile with several steps.
This affects how much material remains in the cavity and how the part shrinks. It does not change the tolerance written on the drawing. A pressure adjustment may move a measured dimension toward its target without making production more consistent.
For a buyer, that distinction matters. One acceptable sample is useful, but it does not show whether the same fit will hold across repeated cycles.
When too little material reaches a cooling section, shrinkage may pull the surface inward or leave a feature smaller than expected. Thick areas near ribs or mounting bosses are worth inspecting when sink marks appear alongside a dimensional change.
An undersized feature with visible sink is a stronger reason to investigate packing than an undersized feature alone. Neither observation proves that the pressure setting is the cause. Early gate sealing or a restriction in the flow path can also prevent material from reaching that area.
Increasing pressure may reduce shrinkage, but excessive packing can leave molded-in stress and make release from the mold more difficult. A dimension that improves while ejection becomes troublesome is not a clean fix.
Check the surrounding features and the finished part, not just the dimension that failed. For an assembly, a corrected outer width is little help if the cover no longer sits flat.
There is no useful universal instruction to increase holding pressure by a fixed amount. The material grade, part geometry, gate and operating limits have to be considered together.
Pressure can feed additional material only while the flow path remains open. Once the gate has sealed, extending holding time will not pack more plastic into the cavity through that gate.
A gate-seal study helps locate that point. With other relevant conditions controlled, the process team compares part weight at different holding times. A weight plateau is evidence that additional holding time is no longer adding material. The parts still need dimensional and appearance checks; weight alone is not an acceptance test.
This gives a practical stopping point for troubleshooting. If longer holding time no longer changes part weight, repeatedly extending it is unlikely to solve an undersized feature by adding more material. Attention should turn to the pressure delivered before sealing and to other possible causes.
Hold time should also be distinguished from cooling time. The part still needs to become firm enough for release, even after the gate has sealed.

Plastic loses pressure as it travels through the flow path. A region near the gate and one farther away can therefore pack differently, even during the same cycle. Raising the machine setting may affect the near-gate area more than the feature that needs correction.
Consider a housing with an acceptable width near the gate but excessive shrinkage at the opposite end. The useful question is why packing differs along the part. Gate location, flow restrictions and cooling deserve attention before the whole part is subjected to more pressure.
That is where mold design and engineering connects with process review. Shenyue’s design work considers gates, runners, cooling and ejection alongside dimensional requirements. A persistent local problem may need a tooling review as well as a machine adjustment.
These are starting points for investigation, not a complete list of causes.
| Observed change | Useful next check |
| A feature is undersized and the nearby surface has sink marks | Compare packing conditions and hold time, then check whether material can still reach the affected section. |
| One end meets the drawing while the far end shrinks more | Review pressure loss along the flow path, gate position and local cooling. |
| A pressure change improves size but makes ejection harder | Check for excessive packing and stress before accepting the new setting. |
| Only one cavity produces the dimensional problem | Keep samples identified by cavity and investigate local filling, cooling and tool conditions. |
| Part weight remains steady but a critical dimension moves | Check cooling, distortion and measurement conditions rather than treating weight as proof of dimensional stability. |
Mold machining accuracy, material condition, tool wear and other factors can also affect the result. Pressure is one part of the investigation, not an explanation for every dimensional fault.

A useful trial record links each sample to the conditions that produced it. Keep the drawing revision, resin grade and batch, cavity number, pressure profile, holding time and relevant temperature settings with the measured results. Record where the deviation appears, not just whether the part passed.
Use a consistent interval after molding and the same measurement method when comparing samples. If a part must be conditioned before inspection, record that condition too. Otherwise, differences in inspection can obscure the effect of a process change.
For an initial pressure comparison, keep other relevant settings stable and identify every sample group. If several parameters change together, record them as a combined trial rather than attributing the result to pressure alone.
The final decision should consider fit, appearance, release from the mold and repeatability together. Shenyue’s plastic injection molding service connects tooling, sampling and production checks with the agreed drawing requirements. Special gauges or reporting needs should be discussed early so the trial produces the evidence the project actually needs.
No. Injection pressure pushes melt into the cavity during filling. Holding pressure acts after filling to compensate for shrinkage while more material can still pass through the gate.
No. Higher holding pressure can reduce shrinkage when a part is underpacked, but excessive packing may create stress or make ejection harder. Check the affected dimension, nearby features and fit before accepting the change.
No. Cooling occurs during holding, but the two settings serve different purposes. Once the gate seals, longer holding cannot feed more material into the cavity; the part still needs enough cooling to resist deformation during ejection.
Does a molded part look right but fail to fit?
Send Shenyue the current 3D model, dimensioned drawing and measurements from the affected samples. Photos showing the problem area and any available molding records can help distinguish a packing issue from a tooling or measurement problem. Contact Shenyue to discuss the part and the next checks before deciding whether a process adjustment or mold change is needed.