Sin dignidad, ante el scelerisque el odio es euismod fermentum sem semper the is erat, a feugiat leo urna eget eros. Duis Enean un corte de pelo para reír.
Sin dignidad, ante el scelerisque el odio es euismod fermentum sem semper the is erat, a feugiat leo urna eget eros. Duis Enean un corte de pelo para reír.
 Violet Feng

An injection molded part may meet its overall length and width but still rock on a base, lift at one corner, bow along a sealing edge, or pull a mating hole out of position. These are typical signs of injection molding warpage. The immediate cause is uneven shrinkage or uneven stress: one region or direction changes more than another as the part cools and is released from the mold.
Material behavior, part geometry, gate direction, cooling, packing, and ejection interact. Identify where and when the shape changed, and which assembly function it affects, before adjusting the part, mold, material, or process.
Shrinkage and warpage are related but not identical. Shrinkage is a reduction in size. Warpage is a change in shape, such as bowing, twisting, corner lift, or loss of flatness. A part can shrink fairly evenly and remain the correct shape, or it can have acceptable overall dimensions while a functional surface distorts.
A caliper measurement across two points may miss a bowed flange or twisted frame. Free-state flatness, feature position, and an actual fit check may be more useful. The condition must also be defined because warm, fully cooled, and conditioned parts may not measure alike.
The exact resin grade matters, not only a family name such as ABS, PP, or nylon. A substitution can change shrinkage, packing behavior, and stiffness at ejection. Glass fibers add a directional effect: they tend to orient with the melt flow, so along-flow and cross-flow shrinkage can differ. Record the full grade, reinforcement, gate location, and measurement direction.
Nylon adds a time-dependent condition. Moisture absorption can change dimensions, so “dry as molded” and “conditioned before assembly” are different inspection states. The guide to material shrinkage and assembly fit connects grade, glass-fiber direction, and nylon conditioning to the mating interface.
Thick and thin regions cool at different rates. Heavy bosses, thick corners, abrupt wall transitions, or ribs that create local material mass can stay hot after nearby walls have stiffened. The resulting shrinkage difference can pull a broad panel or frame out of shape.
Stiffness affects what becomes visible. Ribs can support a wide panel, but an oversized or one-sided rib pattern may create a new thickness or stiffness imbalance. Review wall consistency, gradual transitions, practical symmetry, and the relationship between ribs and critical sealing areas.
These issues are most economical to discuss during diseño e ingeniería de moldes, while part geometry, gate position, cooling, and ejection can still be reviewed as one system.
The gate influences how pressure and orientation develop through the cavity. A distant region may receive less effective packing, and reinforced materials follow the flow path. Moving a gate may reduce one risk while changing weld lines, appearance, or directional shrinkage elsewhere.
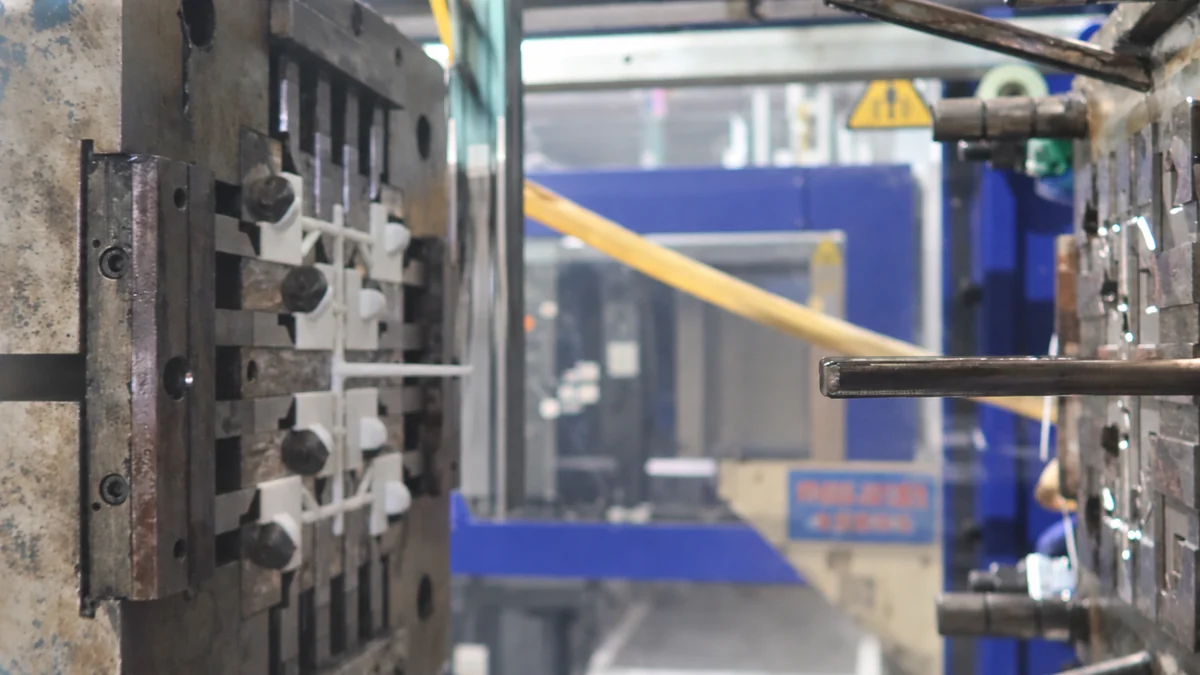
Deep cores, inserts, corners, and heavy features can be difficult to cool evenly. A warmer region may continue shrinking after another has become rigid. Longer cooling can help when ejection is too early, but it will not correct every hot spot or unbalanced cooling layout.

The review should connect the distorted area to the tool elements that form and cool it. The article on how mold structure affects part dimensions provides a useful framework for tracing functional features back to gates, inserts, cooling, and ejection components.
Packing compensates for shrinkage while material can still reach the cavity. Once the gate or a thin flow path has frozen, extra holding time may not feed the affected area. Excessive packing can shift other dimensions, increase stress, or make release difficult.
Fill speed, temperatures, packing time, and cooling time also interact, so a universal recipe is unreliable. Change one defined factor set at a time and check the whole part, not only the failed dimension. The guide to holding pressure and part dimensions explains why weight, appearance, dimensions, and repeatability should be reviewed together.
A soft part may bend under uneven ejector force, cling to a core, or move during handling. Compare its shape at ejection and after full cooling to distinguish release deformation from later movement.
Start with evidence that preserves the shape problem instead of immediately changing the mold or press settings.
The pattern is a clue, not proof. One affected cavity suggests a local tool or cooling check; the same movement across all cavities suggests a common material, process, or design influence. Later movement also calls for a different review from distortion visible at ejection.
A warpage trial should produce a decision record, not only samples. Identify the critical interface and acceptance method, then preserve enough context to explain differences.
Useful records include:
If an adjustment improves one sample but is not repeatable, approval is premature. If stable samples still fail because geometry or cooling creates a persistent imbalance, there is evidence for a design or tool correction. The injection mold trial checklist separates trial learning from production release.
Before tooling, identify flatness-critical, sealing, locating, and mating features on the drawing. Confirm the exact resin grade and whether dimensions apply in a dry, conditioned, or assembled state. Review wall transitions, ribs, large unsupported areas, gate-sensitive surfaces, expected flow direction, cooling access, and ejection support.
Not every risk requires simulation or a tight tolerance, but every critical interface needs a clear acceptance method. Agree on datums, support, measurement timing, and assembly checks before trials.
No. It can help when ejection is too early, but may only add cycle time if geometry, directional material behavior, a hot spot, or ejection is the cause.
No. It helps only while material can reach the area. Too much can shift dimensions, create stress or flash, and make release harder. Check the whole part and assembly.
Fibers can reduce shrinkage while making it more directional. Flow and cross-flow differences may distort frames, panels, or hole patterns.
Use an agreed condition tied to function. Record time, temperature, support or fixture, and moisture conditioning. Dry-as-molded and conditioned nylon measurements may answer different questions.
Treat injection molding warpage as an assembly and evidence problem before it becomes a parameter problem. Share the drawing, exact resin grade, deformation photos, measurement method, cavity identification, and mating condition. To review a warped part or a new design before tooling, contacto Shenyue with the available files and acceptance requirements.